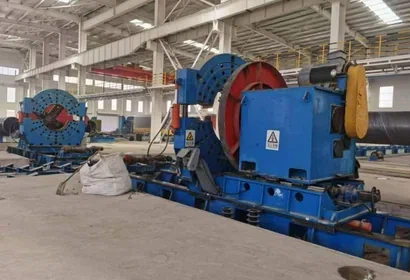
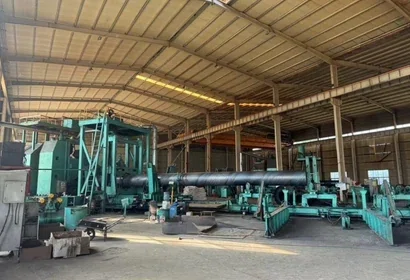
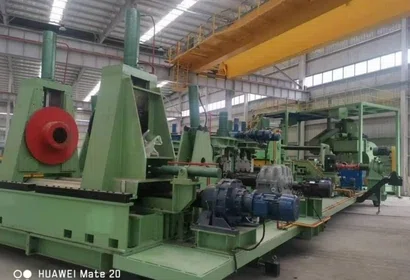
Double Station Chamfering Machine for Steel Pipe Specification
| Flat head speed | 12-18 pieces/minute |
| Flat head machine cutter head motor | 7.5KW, 6-stage, 2 units (equipped with two frequency converters) |
| Stepping power | 7.5KW, Level 4, 1 set (equipped with a frequency converter) |
| Pushing motor | 0.37KW, Level 4, 1 unit |
| Feed method | Servo motor feed |
| clamping system | The clamp adopts an asymmetric design, with the lower clamp designed at 10 degrees to ensure accurate entry of the steel pipe into the flat head position. The upper clamp designed at 60 degrees is more conducive to clamping. |
| Stepping system | The stepper system adopts a counterweight design and a double gear box structure. Variable frequency speed regulation to achieve fast stepping and adapt to various pipe flat head speed requirements |
Double Station Chamfering Machine for Steel Pipe Equipment Composition
1. Electronic control system
The operation of the automatic system is controlled by PLC, and the walking beam adopts frequency conversion speed regulation to control the stepping speed.
The main control cabinet includes PLC, frequency converter and relay control system, and an operation console is convenient for operation. It adopts stainless steel panel and 2 operating tables.
2. Mechanical system
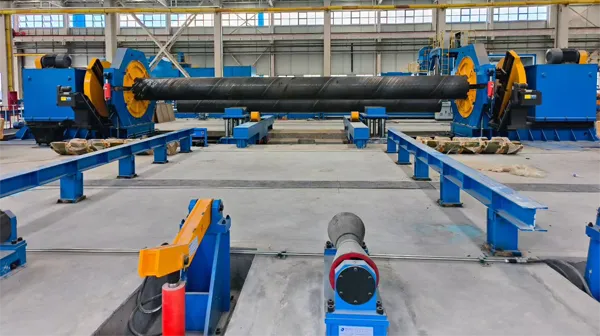
1) Feeding system (2 sets);
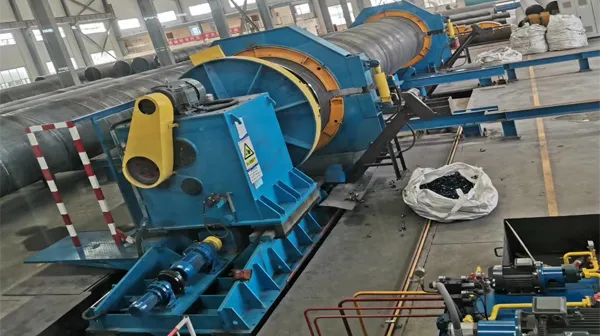
2) Steel pipe flat head support and clamping system (2 sets on each side);
3) Cutter spindle power head and drive motor system (2 sets);
4) Walking beam management and step transfer system (3 lanes, 1 set);
5) Fixed fork positioning system (3 channels, 1 set);
6) Double-pipe pushing roller table and baffle system (2 sets).
Double Station Chamfering Machine for Steel Pipe Work Process
This pipe chamfering machine adopts PLC to control the actions of automatic pipe division, step-by-step transfer, clamping, feeding and retracting, pushing and other actions, and the left and right dislocations are flat or the two sides are aligned.
The pipe branching system first dials in two pipes and automatically separates them into two pipe slots.
After the automatic left push, step into the double station again to enter the right cutter head, the right automatically clamps, feeds, retracts, releases the clamp, and then steps into the double station.
After the automatic right push, step into the double station again to enter the left cutter head, the left automatically clamps, feeds, retracts, and releases the clamp, and then steps into the double station, and the outlet pipe enters the packaging.
During automatic continuous operation, actions such as flattening, clamping, feeding, retracting, and unclamping are simultaneously performed on the left and right sides.