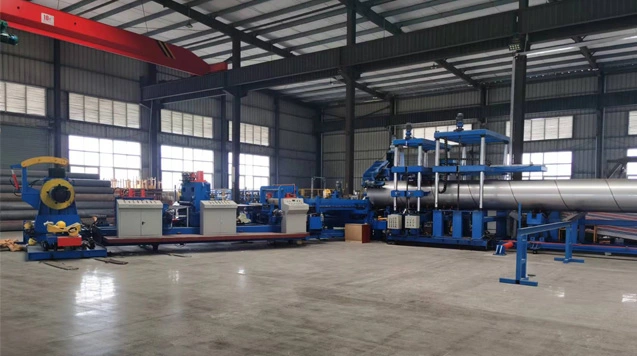
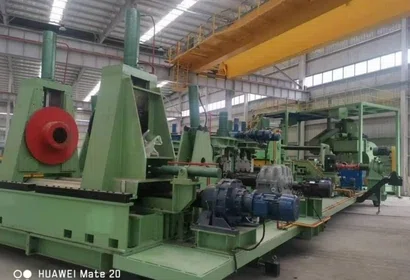
Thin Wall Spiral Welded Pipe Production Line Unit Process
Uncoiling→head removal→lead material leveling→vertical roll alignment→shear butt welding→vertical roll alignment→delivery→guide plate pressing→forming→internal welding→cutting→steel pipe output.
Molding process introduction
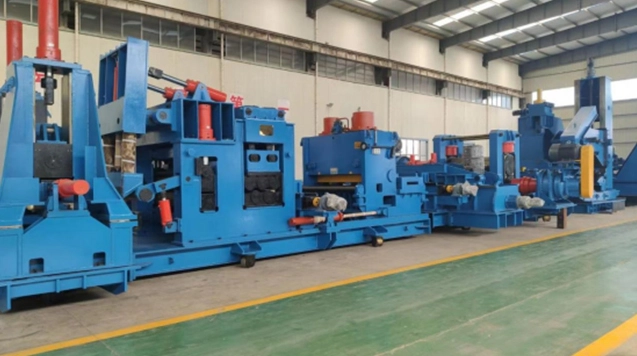
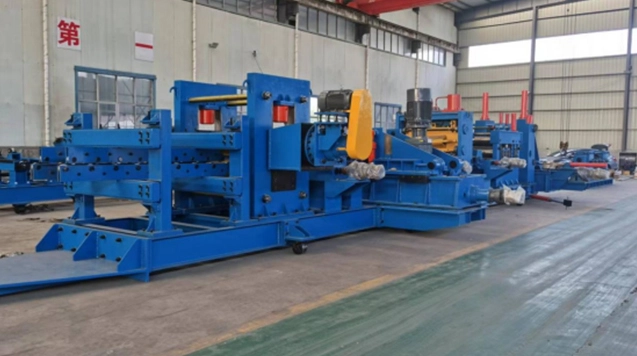
Firstly, the steel coil is hoisted to the supporting base of the coiler by the crane, transported to the coiling center of the uncoiler, and the coil is tightened by the coiling inner support, and the steel coil can be accurately moved to the center of the required delivery line through the operation button, and then the pressure roller is operated to compress the steel coil, and the motor is started to rotate the steel coil. After the strip head enters the pinch roller, the pinch roller is pressed down and the strip steel is forwarded, and the strip steel is leveled by the leveling roller, and the strip steel continues to move forward, and the head and tail of the strip are cut by hydraulic shears, and the front and rear steel coils are connected by manual secondary welding, and the vertical roller ensures that the strip steel is on the delivery center line. Afterwards, the strip steel enters the delivery machine, which is the main power source of the screw welding unit. It is used to generate forming force and overcome various resistances, such as uncoiling resistance, leveling resistance, forming resistance, etc., and the strip steel is sent into the former. The 1#, 2#, and 3# forming rollers of the former are forced to deform the steel plate to form a steel pipe. The spiral welded pipe is equipped with an automatic length-setting and steel pipe cutting device on the rear axle, which cuts the steel pipe according to the required length during the production process to ensure the continuous production of the unit.
According to the forming theory, in the production process of spiral welded pipe, the rear axle angles corresponding to different steel pipe diameters are also different, and the corresponding relationship is shown in the following formula:
cosα=1500/πDm
Where: α is the forming angle
1500 is the width of the steel plate
Dm is the middle diameter of steel pipe, Dm=D (outer diameter of steel pipe)-t (thickness of steel plate)
In actual production, the required forming angle can be calculated according to the above formula, and then the rear axle can be adjusted to a suitable position according to the calculated value, and the forming roller can be adjusted to a suitable position before starting production.
Thin Wall Spiral Welded Pipe Production Line Equipment Composition
| Equipment name | Quantity (set) |
| Uncoiler | 1 |
| Roller | 1 |
| Vertical roll | 1 |
| Electric Vertical Roller | 2 |
| delivery machine | 1 |
| Guide plate | 1 |
| Forming machine | 1 |
| Front axle unit | 1 |
| Internal welding device | 1 |
| rear axle unit | 1 |
| Gantry Centralizer | 1 |
| output bay | 1 |
| Cutting trolley | 1 |
| Front and rear axle embedded parts | 1 |
| hydraulic system | 1 |
| Electronic control device 1 | 1 |